A detailed Import/Wholesale Guide is the only barrier between a profitable shipment and a container full of unsellable inventory. The price difference between an “A-Grade” and “B-Grade” vanity looks tempting on a quote sheet, but that small saving evaporates when you account for warped doors, cracked paint, and misaligned joints. One bad container doesn’t just destroy your margin; it can damage your reputation with builders and retail partners who depend on your quality control.
This checklist serves as a technical standard operating procedure for your team or third-party inspectors on the factory floor. We will cover the essential on-the-ground checks, from measuring wood moisture content to prevent warping, to verifying joint construction and finish flatness. You will also learn how to interpret packaging drop test standards like ISTA 3A, analyze supplier quotes for hidden risks, and direct proper container loading logic to protect your investment all the way to your warehouse.
The Risks of Global Vanity Sourcing
Sourcing bathroom vanities globally looks cost-effective on paper, but the real risks are found in specification drift, volatile lead times, and compliance failures that erase initial savings.
Quality Control and Specification Mismatches
Sourcing from distant factories often creates a gap between the specified design and the final product. Without direct, on-the-ground oversight, factories can substitute materials or cut corners on manufacturing standards, directly impacting the vanity’s durability and aesthetic. This isn’t a theoretical problem; it happens constantly.
- Receiving products made with inferior materials, like low-grade plywood that isn’t moisture-resistant or PVC sheets below the specified density.
- Final paint or laminate finishes that fail to match the approved Pantone specifications or physical control samples.
- Hardware such as hinges and slides failing prematurely because the factory used uncertified, low-cost components to save a few dollars per unit.
Supply Chain Disruptions and Lead Time Volatility
Global supply chains are inherently vulnerable. Port congestion, customs clearance issues, and unforeseen production pauses are now standard operating risks. These disruptions extend project timelines and create critical inventory shortages for distributors who depend on predictable stock flow.
- Unexpected production delays at the factory level that push project schedules back by weeks or even months.
- Shipping and logistics bottlenecks that can double expected lead times without any warning.
- A fundamental lack of real-time visibility into where an order actually is in the production and transit cycle.
Navigating Regulatory and Compliance Hurdles
Each target market has unique, non-negotiable standards for safety, materials, and environmental impact, such as UL in North America or CE in Europe. Working with a factory that doesn’t understand or prioritize these regulations is a direct route to having your products seized at the border, facing fines, or being unable to legally sell your inventory.
- Products being rejected by customs because integrated electronics, like in LED mirrors, fail to meet local electrical standards.
- Materials containing formaldehyde levels that exceed regional emissions limits like CARB 2.
- Designs that do not meet specific accessibility or water-efficiency requirements, like ADA or WELS.
Hidden Costs and Geopolitical Instability
The initial quote from a supplier rarely reflects the total landed cost. Unforeseen tariffs, currency fluctuations, and unexpected shipping fees can inflate expenses significantly. Beyond logistics, geopolitical tensions can suddenly impact trade routes, material availability, and a factory’s ability to operate.
- Unforeseen tariffs or import duties that increase the final cost per unit after the order has already been placed.
- Fluctuating currency exchange rates that erode profit margins between the time of deposit and final payment.
- Supplier operations being impacted by regional lockdowns or sudden trade policy changes that halt production entirely.
Critical QC Points: Finish, Joints, & Flatness
A vanity’s longevity isn’t determined by its design, but by the microscopic integrity of its surfaces, seams, and dimensions—defects here guarantee failure.
Beyond a simple visual inspection, a robust Quality Control process for bathroom vanities relies on verifiable data points. The difference between a product that lasts two years and one that lasts ten is found in the disciplined evaluation of its finish, the strength of its joinery, and the precision of its dimensions. These three areas are non-negotiable checkpoints for any serious importer or wholesaler.
Surface Finish Inspection
The finish is the vanity’s first line of defense against moisture and wear. A proper inspection confirms the coating is not just aesthetically pleasing but also functional and durable. This process moves beyond subjective looks to objective performance metrics, ensuring the protective layer will not fail prematurely under typical bathroom conditions. Any inconsistencies in thickness or adhesion are immediate red flags for long-term problems like peeling or bubbling.
- Visual checks for cosmetic perfection under controlled, high-intensity lighting.
- Adhesion tests (like cross-hatch testing) to confirm the coating will not peel or flake.
- Digital thickness measurements to ensure a consistent and sufficient protective layer.
Joint and Seam Integrity
Structural integrity begins where two components meet. Every joint, seam, and connection point is a potential point of failure if not perfectly executed. Inspections in this area focus on the strength and alignment of all structural bonds, from cabinet corners to door frames. A perfectly sealed and flush joint not only looks better but is critical for preventing water ingress and maintaining the cabinet’s rigidity over years of use.
| Material | Finish Type & Key QC Checks | Common Failure Points |
|---|---|---|
| High-Density PVC | High-Gloss Lacquer or PVC Skin (Membrane). Checks focus on color uniformity, adhesion (no bubbling), and consistent sheen. | Orange peel texture in lacquer, delamination of PVC skin at edges, color mismatch between batches. |
| Water-Resistant Plywood | High-Pressure Laminate/Melamine or PU Painting. Checks include edge banding integrity, laminate surface flatness, and paint layer thickness. | Chipped edge banding from improper cutting, visible seam lines, inconsistencies in wood grain pattern. |
| HMR MDF | Primarily used for ultra-smooth High-Gloss Lacquer. QC requires multi-layer surface purity inspection before painting to prevent imperfections. | Minor surface flaws (“telegraphing”) showing through the gloss finish, poor moisture sealing at cutouts or edges. |
- Analysis of bonded or screwed joints for complete fusion and strength.
- Verification that mechanical fasteners are torqued to correct specifications without stripping or material damage.
- Inspection of seams to ensure they are flush, sealed, and visually clean.
Flatness and Dimensional Accuracy
Modern manufacturing relies on precision. A vanity that isn’t perfectly flat and dimensionally accurate will cause significant installation problems. Doors may hang crooked, drawers might not align, and countertops can crack when installed on a warped cabinet base. Using precision tools like digital calipers and laser levels, this check guarantees that every component matches the design blueprint within strict tolerances. This prevents assembly issues on-site and ensures a clean, professional final installation.
- Measurement of all large surfaces (tops, sides, doors) to detect any warping or bowing.
- Confirmation that overall product dimensions are within the specified tolerance range (e.g., +/- 1mm).
- Verification of critical component geometry, such as squareness of corners and placement of drill holes.
Factory-Direct Vanities Built for Your Market
Moisture Content Checks (Crucial!)
Failing to manage wood moisture content for the destination climate is the primary cause of warping, joint failure, and finish degradation in globally shipped vanities.
Why Wood Warps: The Science of Moisture
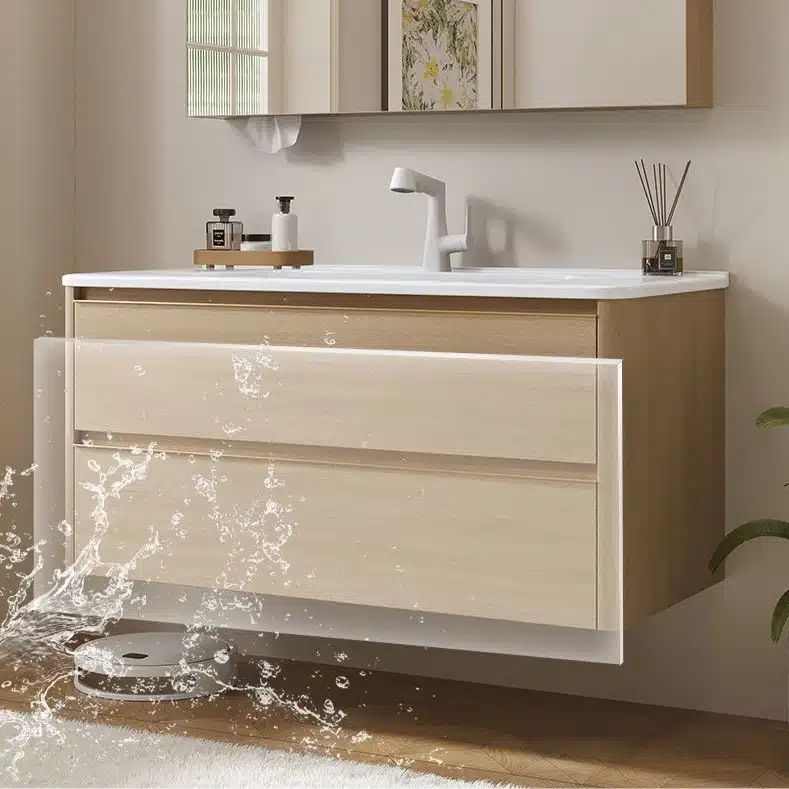
Wood is a hygroscopic material, which means it naturally absorbs and releases moisture to balance with the air around it. When this internal moisture content is out of sync with the ambient environment, wood expands or contracts unevenly. This movement is the direct cause of warping, cracking, and joint failure in finished cabinets. Uncontrolled moisture makes wood fibers swell or shrink, compromising the vanity’s structural integrity. This is a critical failure point for products shipped across different climate zones, from humid ports to dry inland cities. Properly dried and sealed wood holds its shape, ensuring doors and drawers function correctly for years.
Standardized Testing Methods (Gravimetric & NIR)
We use multiple industry-standard techniques to verify wood moisture content before any material enters production. These methods give us precise, data-driven assurance that all lumber meets strict quality benchmarks for long-term stability. Gravimetric testing provides a baseline for accuracy by measuring material weight before and after kiln drying. For real-time checks, Near-infrared (NIR) spectroscopy offers a non-destructive way to scan raw materials as they arrive from suppliers. This dual-method approach confirms compliance and drastically reduces the risk of substandard lumber ending up in a finished product.
Climate-Specific Moisture Targets
A single moisture content target doesn’t work in a global market. We calibrate moisture levels based on the destination region’s average humidity. This “region-ready” strategy is key to preventing defects after installation. Materials destined for humid regions like Oceania are prepared to a lower moisture content to minimize swelling after arrival. Conversely, wood intended for arid climates in the Middle East or parts of North America is processed to hold slightly more moisture to prevent cracking. By 2025, our production lines will integrate real-time climate data to automate these calibrations for every order.
| Climate Zone | Typical Relative Humidity (RH) | Target Wood Moisture Content (MC) |
|---|---|---|
| Humid (e.g., Oceania, SE Asia) | 65%+ | 6% – 8% (Prevents swelling) |
| Temperate (e.g., Europe, North America) | 40% – 60% | 8% – 9% (Balanced for stability) |
| Arid (e.g., Middle East, SW USA) | < 40% | 9% – 10% (Prevents cracking) |
Impact on Long-Term Durability and Finish
The correct moisture content is fundamental to the vanity’s finish and overall lifespan. Excess moisture trapped beneath paint or sealant leads directly to bubbling, peeling, and premature failure. Paint and lacquer can only adhere properly to wood with a stable moisture level, which is necessary for a smooth, lasting surface. Trapped moisture also creates a breeding ground for mold or mildew inside the wood—a major problem in any bathroom. Verifying moisture content is not just about structure; it protects the final finish and is essential for guaranteeing the product’s durability for a decade or more.
Packaging Drop Tests (ISTA Standards)
Standardized drop testing is no longer optional; it’s a mandatory pre-shipment inspection for any brand selling vanities online, as it directly reduces costly transit damage and return rates.
Simulating Real-World Transit Conditions
International Safe Transit Association (ISTA) tests are designed to replicate the specific shocks, drops, and impacts a package will face during global shipping. This proactive approach identifies potential packaging failures before a bathroom vanity or smart mirror ever leaves the factory. By 2025, the primary goal of these simulations is to slash transit damage claims by exposing these vulnerabilities early. The test protocols are even tailored to mimic specific routes, from factory loading in Asia to final last-mile delivery in North America or Europe.
The ISTA 1A Procedure
The ISTA 1A procedure has become the industry benchmark for pre-shipment inspection. It provides a standardized, repeatable framework for basic drop testing, making it a reliable quality check recognized by third-party inspectors and logistics partners. This test is a fundamental step in quality assurance for international orders. It involves a strict sequence of ten controlled drops that target the package’s most vulnerable points: its faces, edges, and corners. While 1A is a solid baseline, our e-commerce packaging is built to pass the more rigorous ISTA 3A standard required by major platforms like Amazon and Wayfair.
Core Methods: Freefall and Rotational Impact
The main assessments within the ISTA 1A test are freefall drops from a set height and rotational drops to check edge and corner strength. These actions simulate the most common and damaging events that occur during manual handling and automated sorting. The drop height is calibrated based on the total weight of the package, applying realistic stress. Rotational tests are especially critical for heavy or long items like sintered stone countertops, which can suffer severe corner damage if they are tipped or mishandled during loading.
Advanced Testing: Vibration and Compression
For high-value or fragile shipments, testing protocols often extend beyond simple drops. Vibration and compression tests are added to simulate the constant rattling on a truck or ship and the immense pressure of being stacked inside a shipping container. Vibration tables identify risks of internal scuffing, loose hardware, or detached mirror brackets. Compression tests verify that a package can support the weight of others stacked on top without crushing, a critical factor for optimizing container space and ensuring the bottom-layer products arrive intact.
Analyzing “B-Grade” vs. “A-Grade” Quotes
The core difference between A-Grade and B-Grade products is cosmetic, not functional, creating a strategic opportunity for importers to serve different market segments without sacrificing product reliability.
Understanding the distinction between “A-Grade” and “B-Grade” is critical when evaluating quotes from overseas factories. These terms aren’t arbitrary; they represent a standardized classification used across wholesale markets to define product condition. Getting this wrong leads to disputes and inventory that doesn’t match market expectations.
Defining the Grade: Functional vs. Cosmetic Standards
The primary distinction is simple: A-Grade products are in perfect cosmetic condition, while B-Grade items are fully functional but have minor, non-structural imperfections. These flaws could be small scratches, slight color variations, or minor dents that occurred during production or handling. Both grades must pass the same performance and operational benchmarks. The imperfections in a B-Grade vanity do not affect its lifespan, structural integrity, or usability. A-Grade simply guarantees flawless aesthetics suitable for high-end residential projects or showroom displays.
| Attribute | A-Grade (Showroom Quality) | B-Grade (Functional Quality) |
|---|---|---|
| Operational Integrity | Passes all functional QC checks. | Passes all functional QC checks. |
| Cosmetic Condition | Flawless. No visible scratches, dings, or discoloration. | Minor, non-structural imperfections (e.g., small scratches, slight paint blemishes). |
| Ideal Market | Luxury homes, retail showrooms, high-end projects. | Rental properties, commercial spaces, budget-conscious projects. |
Price Discrepancy and Market Positioning
B-Grade quotes are always lower, and that price reduction is a direct reflection of the cosmetic condition—not a drop in material quality or construction. This pricing tier allows distributors to target budget-conscious market segments that prioritize function over flawless looks. For instance, B-Grade inventory is ideal for high-traffic commercial bathrooms, rental properties, or renovation projects where minor blemishes are acceptable. This strategy also enables partners to test new designs or markets with a lower initial investment, reducing financial risk.
Supplier Transparency and Building Trust
A reliable manufacturing partner will have clear, documented standards defining each grade. When analyzing a quote, demand detailed descriptions or reference photos illustrating what constitutes a B-Grade flaw. This transparency is a key indicator of a trustworthy supplier and prevents disputes when the container arrives. We provide detailed QC reports with images for every shipment, ensuring our buyers understand the exact condition of every A-Grade and B-Grade unit before it leaves our factory. This removes ambiguity and aligns expectations from the start.
Container Loading Logic (Top vs. Base)
The choice between top-loading and base floor-loading is a core logistics calculation, balancing the cost efficiency of maximizing space for stackable goods against the specialized access required for oversized or irregular cargo.
Top-Loading for Irregular and Oversized Cargo
Top-loading strategies are the industry standard for any cargo that exceeds the dimensions of a standard container, such as heavy machinery or project-specific materials. This approach uses open-top containers, allowing cranes and other equipment to lower items in from above, bypassing height and width constraints imposed by standard container doors.
- This method is essential for large, non-stackable items like custom-built bathroom installations or oversized stone slabs.
- It simplifies the loading and unloading of heavy equipment that cannot be handled through conventional container doors, reducing labor and potential damage.
Base Floor-Loading for Maximizing Space with Stackable Goods
Base floor-loading is the most cost-efficient and common approach for uniformly packaged, stackable goods like boxed bathroom vanities, mirrors, and hardware. The process involves optimizing container space by building stable, layered tiers directly from the container floor. This technique maximizes the usable cubic volume of the container, directly lowering the per-unit shipping cost.
- This is the preferred method for high-volume shipments of standardized products where maximizing units per container is the primary goal.
- Careful planning is required to ensure weight is distributed evenly across the container floor to maintain structural integrity and prevent shifting during transit.
Choosing Specialized Containers for Unique Needs
Beyond standard dry containers, specialized options provide critical flexibility for unique cargo challenges. Flat racks and open-tops solve dimensional problems that would otherwise make shipping impossible. These containers ensure structural integrity for any type of shipment, accommodating loads that are too wide or too tall for conventional methods.
- Flat racks are designed without side walls and are ideal for cargo that extends beyond the sides of a traditional container.
- Open-top containers use removable tarpaulin coverings, offering protection from the elements while still allowing for easy top-loading access.
Inspecting Hardware (Hinges/Slides)
Hardware quality control is no longer just a visual check; it’s a structured process combining visual, mechanical, and material validation to meet established ANSI/BHMA standards and prevent field failures.
Visual Assessment of Finish and Alignment
A visual check confirms that the hardware’s appearance and installation meet quality standards. This is the first step in identifying surface-level defects that can indicate deeper manufacturing issues. Poor alignment or inconsistent finishing often points to a lack of process control at the factory level.
- Inspect all surfaces for scratches, rust, plating defects, or discoloration.
- Ensure screws are tight and hinges or slides are properly aligned, with no sagging or uneven gaps.
- Verify that the finish (e.g., chrome, brushed nickel) is consistent across all pieces.
Functional Performance and Mechanical Testing
This hands-on test evaluates the mechanical operation of hinges and slides to ensure they function smoothly and reliably, reflecting standards set by organizations like ANSI and BHMA. Subpar action is a direct indicator of poor internal components or incorrect assembly. The hardware must perform without friction or noise under normal operating conditions.
- Open and close drawers and doors multiple times to check for smooth, quiet action.
- Confirm that soft-close mechanisms engage correctly without slamming or requiring force.
- Test for any sticking, grinding, or excessive play in the hardware’s movement.
Corrosion Resistance and Material Validation
Validating material durability is critical for long-term product reliability, especially for vanities intended for humid bathroom environments or international shipping where container conditions can vary. Reputable manufacturers offer hardware upgrades from standard soft-close systems to premium brands like DTC or Blum, which come with documented performance metrics and superior corrosion resistance.
- Review manufacturer documentation for salt spray test results or other corrosion resistance certifications.
- Check that the hardware material specified in the order (e.g., stainless steel grade) matches the delivered product.
- Assess for early signs of rust or degradation, particularly at joints and mounting points.
Conclusion
Moving beyond the initial FOB price to inspect moisture content, finish quality, and packaging is essential. These details directly impact product longevity and customer satisfaction. A disciplined quality control process protects your brand reputation and prevents expensive rework or returns.
Use this checklist to evaluate your current import strategy and identify potential gaps. For a practical demonstration of these quality standards, you can request a detailed quote or a refundable sample for your review.
Frequently Asked Questions
What is the ideal moisture content for wood vanities?
The ideal moisture content (MC) for solid wood and wood-based components in bathroom vanities is between 6% and 9%. This range ensures the wood is properly acclimatized for a typical indoor home environment, minimizing the risk of warping, cracking, or joint failure after installation. Maintaining this MC level from manufacturing through shipping is critical for long-term product stability.
How to check for paint quality on cabinets?
A thorough paint quality check involves three steps. First, perform a visual inspection under good lighting, looking for a smooth, consistent finish free of drips, sags, “orange peel” texture, or dust particles. Second, check for color consistency across all components. Finally, test for adhesion using a cross-hatch test (a simplified version of ASTM D3359), where you score a small grid into the paint in an inconspicuous area and apply strong tape to see if the finish peels off. A quality finish will show minimal to no paint removal.
What is the ISTA 3A packaging standard?
ISTA 3A is a testing standard from the International Safe Transit Association designed to simulate the shipping environment for individual packaged products under 150 lbs (70 kg) sent through a parcel delivery system like UPS or FedEx. The test protocol includes a series of drop tests from various heights and angles, random vibration tests under load, and atmospheric conditioning to ensure the packaging can protect its contents from the typical shocks, drops, and pressures of small parcel handling.
How to prevent mold inside shipping containers?
Preventing mold requires strict moisture control. The primary method is to use industrial-grade desiccants (e.g., calcium chloride bags) inside the container to absorb ambient humidity and prevent “container rain” or condensation. Additionally, ensure products and any wood pallets are dried to their target moisture content before loading. The container itself should be inspected to be clean, dry, and free of leaks before sealing. For extremely sensitive cargo, a sealed container liner can provide an extra barrier.
Should I import tops and cabinets separately?
Yes, it is the industry best practice to import vanity tops and cabinets separately. Shipping heavy stone tops packaged in the same box as the wood cabinet base is a leading cause of damage during transit. Separating them dramatically reduces the risk of cracked tops and crushed cabinets. While it adds logistical complexity, this method provides superior protection, allows for greater inventory flexibility, and is the standard procedure for professional, high-volume importers focused on quality control.
Common defects in Chinese vanity imports?
Common defects often fall into four categories. 1) Finish Quality: Inconsistent paint sheen, drips, orange peel texture, and poor adhesion. 2) Construction: Misaligned doors and drawers, weak joinery (improper gluing or doweling), and use of low-quality hardware. 3) Material: High wood moisture content leading to warping, substitution of specified materials (e.g., using MDF instead of plywood), and visible blemishes. 4) Countertops: Hairline cracks, chips, poor polishing, and color variations not consistent with natural stone patterns.
0 Comments